Modernize industrial operations with Industry 4.0 and IoT
Connect equipment, systems and production data with IoT, digital twins and smart factory solutions that improve visibility, reduce downtime and support scalable automation.
Measurable impact across smart industrial operations
Technology partner
Lower energy use. Smart metering and IoT monitoring help identify consumption patterns and optimize equipment usage.
Greater operational visibility. Connected sensors and real-time dashboards provide clearer insight into equipment, production and OEE.
Less unplanned downtime. Predictive maintenance and condition monitoring help identify issues before they interrupt operations.
Faster issue response. Real-time alerts and diagnostics help teams detect disruptions earlier and respond more quickly.
How we modernize connected industrial operations
From factory automation and digital twins to connected logistics, we integrate equipment, data and workflows to improve visibility, reliability and operational control.
Industry 4.0 and factory automation
Connect machines, production systems and workflows with IoT, analytics and automation. Improve overall equipment effectiveness (OEE), process visibility and quality while creating a foundation for scalable smart manufacturing.
IoT and digital twin integration
Connect physical assets with real-time sensor data and digital models to monitor conditions, simulate outcomes and optimize equipment and production performance.
Supply chain and logistics digitalization
Improve inventory, warehouse and logistics visibility with connected systems, real-time tracking and automated workflows from source to delivery.
Turn Industry 4.0 into measurable business value
Connect manufacturing, FMCG and logistics operations through IoT, intelligent automation and real-time data. From the factory floor to last-mile delivery, we help improve efficiency, visibility and operational resilience.
AI-driven control for smarter production
Predictive maintenance and condition monitoring
Detect equipment issues earlier using real-time sensor data and AI-assisted monitoring. Reduce unexpected downtime and improve maintenance planning with actionable equipment insights.
Automated quality inspection
Use computer vision and AI-assisted inspection to identify defects in real time, improve quality consistency and reduce manual inspection across production lines.
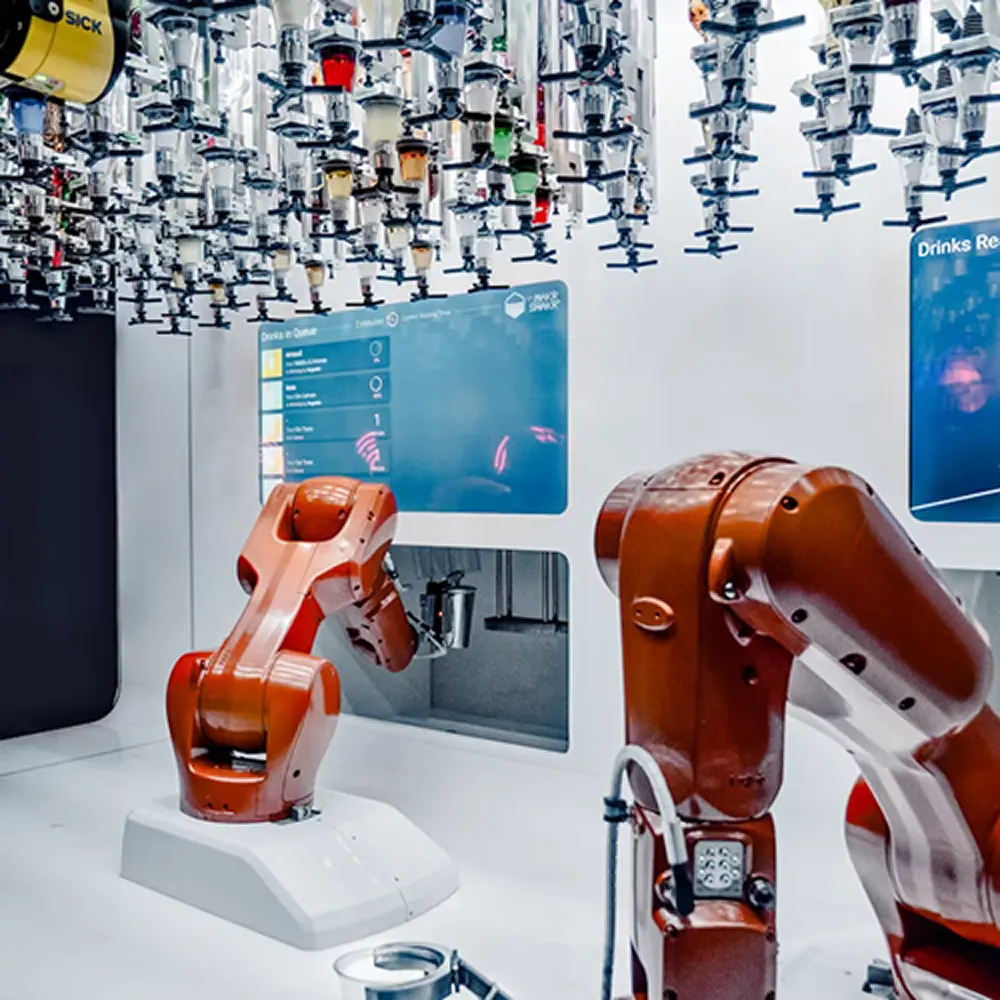
Connected assets with real-time visibility and optimization
Digital twin simulation and live monitoring
Create digital models of machines and operating environments to monitor performance, simulate changes and evaluate outcomes before applying them to live operations.
IoT sensors and edge intelligence
Capture equipment and environmental data at the edge to monitor temperature, vibration, throughput and other critical conditions while enabling faster local responses.
Connected logistics from source to delivery
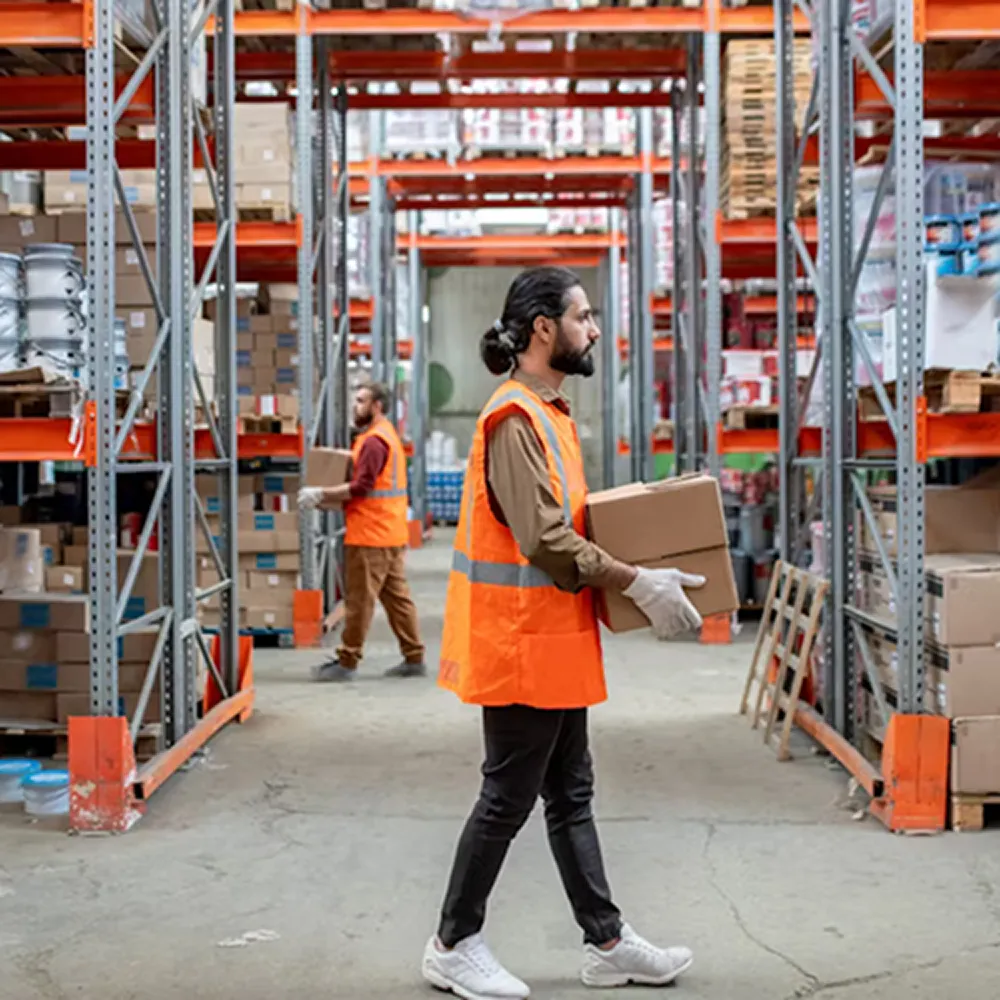
Smart inventory and warehouse automation
Connect inventory, warehouse and fulfillment operations with real-time tracking, automated workflows and intelligent inventory controls to improve accuracy and throughput.
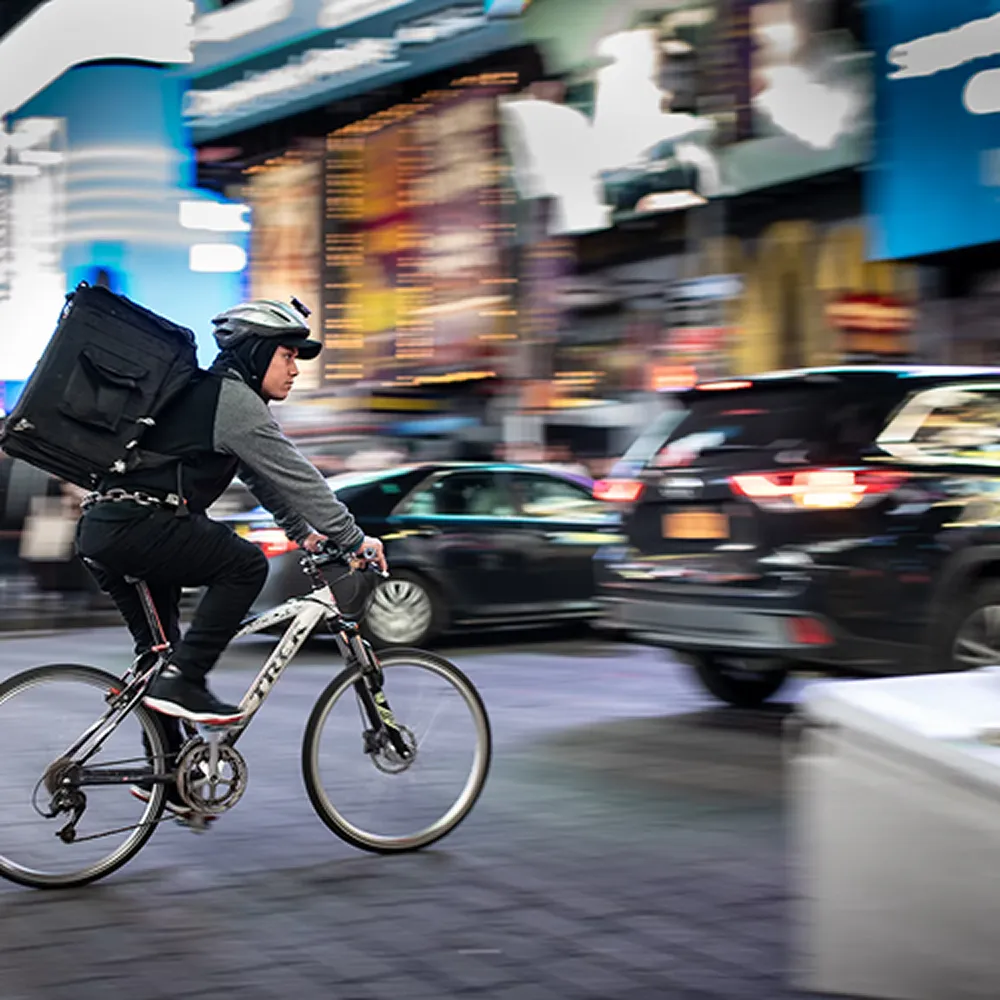
Intelligent routing and delivery visibility
Monitor vehicles, delivery status and route performance in real time. Use data-driven scheduling and alerts to respond faster to delays, demand changes and operational disruptions.
Smarter decisions from production to shelf
Demand-driven inventory and replenishment
Combine sales data, demand trends and predictive analytics to optimize stock levels across warehouses, distribution centers and retail locations while improving product availability.
Connected omnichannel operations
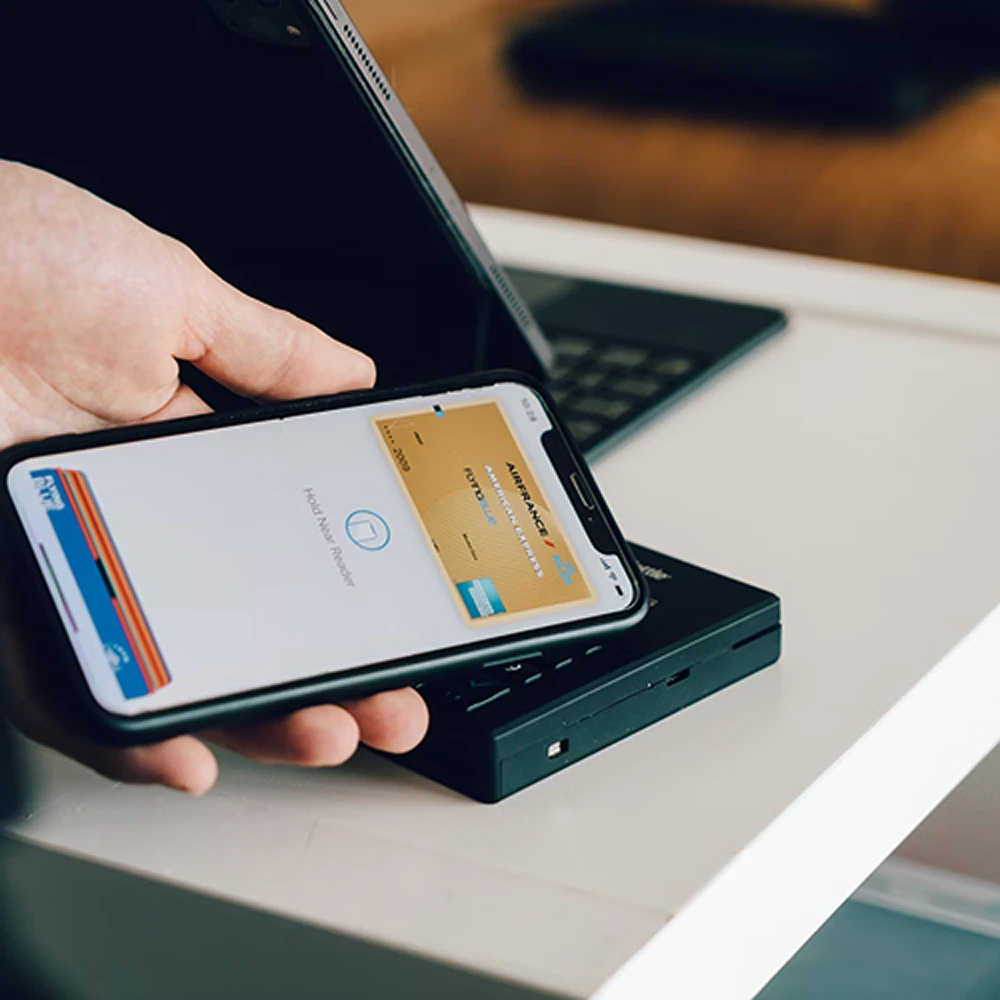
Integrate POS, e-commerce, CRM and enterprise systems to connect online and offline operations, improve customer visibility and support consistent experiences across channels.
Technology powering connected industry operations
We connect enterprise, logistics, commerce and operational platforms to build integrated digital ecosystems that improve visibility, automate processes and scale across your value chain.